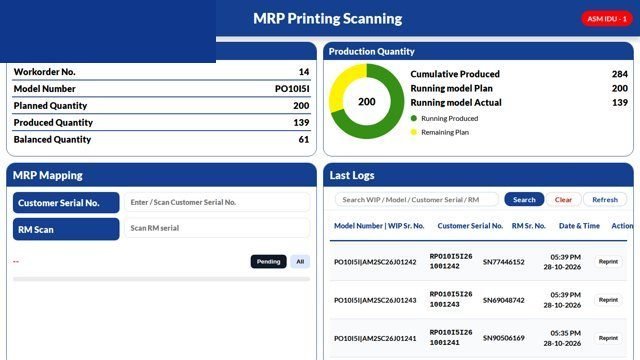
Every unit scanned at every station. Nothing skips a stage.

Each unit carries a serial. At every station MOS checks that the unit passed every stage before it, that the parts fitted match the bill of materials, and that the test results are within limits — and only then lets the line move on. Labels print at the right station, quality holds stop a batch on the spot, and every unit keeps its full history from first station to the truck.
Stations, their order, the parts fitted at each and the tests each must pass are set up once; a planner releases a work order and every station gets the model's masters.
The unit serial is scanned; MOS checks it passed every earlier stage and fits the right parts.
Leak, vacuum, hi-pot and run-test results are read from the benches — not typed.
Only a unit that passed everything gets its label and moves on; a quality hold stops a batch at once.
Every figure comes from the machine, the camera or the station itself — recorded as it happens, not typed in at the end of the shift.
A clear go / no-go at the station, with the reason
Holds, releases and every test result by serial
Output per station and hour, first-pass yield
Only released units, matched and labelled
A scanner, and a screen or tablet for the go / no-go.
The bench result read over its network or from its files.
The MOS plant server and label printers where labels are applied.
Stations, order, parts and tests set up with your team.
Stations scan and refuse units that skipped a stage.
Every unit traceable from first station to truck.
The station keeps its last state and the plant server runs locally; scans are queued and posted when the link returns.
Only a role you allow can release a held unit, and every release is recorded with who and why.
Every machine, live — and the real reason it stopped.
See the module →kWh per machine, per shift and per part — read from the meters, not the bill.
See the module →Every part judged by camera in under a second, defect circled.
See the module →Tell us about your plant and what you want to see. We visit, connect one machine or station, and you watch your own data in MOS before anything is quoted.