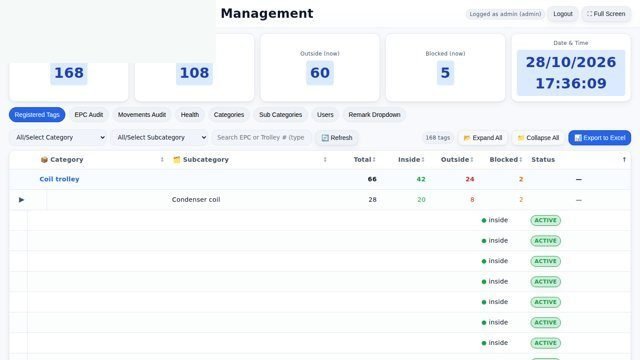
Every trolley, every gate, every movement — on its own.

Tagged trolleys and assets are read automatically as they pass a gate. MOS knows which way they moved, lights the tower lamp green, red or orange through the gate PLC, holds back blocked trolleys with a countdown and an approval workflow, and keeps an audit of every movement.
Each trolley or asset carries a UHF tag registered to its type and route.
Two readers per gate tell in from out as the trolley passes.
The gate PLC lights the tower lamp green, red or orange at once.
A blocked trolley starts a countdown and an approval workflow; every move is audited.
Every figure comes from the machine, the camera or the station itself — recorded as it happens, not typed in at the end of the shift.
Instant lamp and reason at the gate
Where every trolley is now
Movements per gate and shift
Breaches and how fast they were closed
Two UHF readers to tell in from out, and a tower lamp.
A UHF tag on every trolley, pallet or bin.
The gate PLC or a relay box, and the MOS plant server.
One gate live with its lamp.
Register built; movement rules set per route.
Approvals, breaches and audit running plant-wide.
On-metal tags are used for metal assets; reader placement is tuned at the gate during installation.
It is flagged at the gate and must be confirmed before it is counted.
Know what is on every rack before anyone walks there.
See the module →Every machine, live — and the real reason it stopped.
See the module →Every unit scanned at every station. Nothing skips a stage.
See the module →Tell us about your plant and what you want to see. We visit, connect one machine or station, and you watch your own data in MOS before anything is quoted.