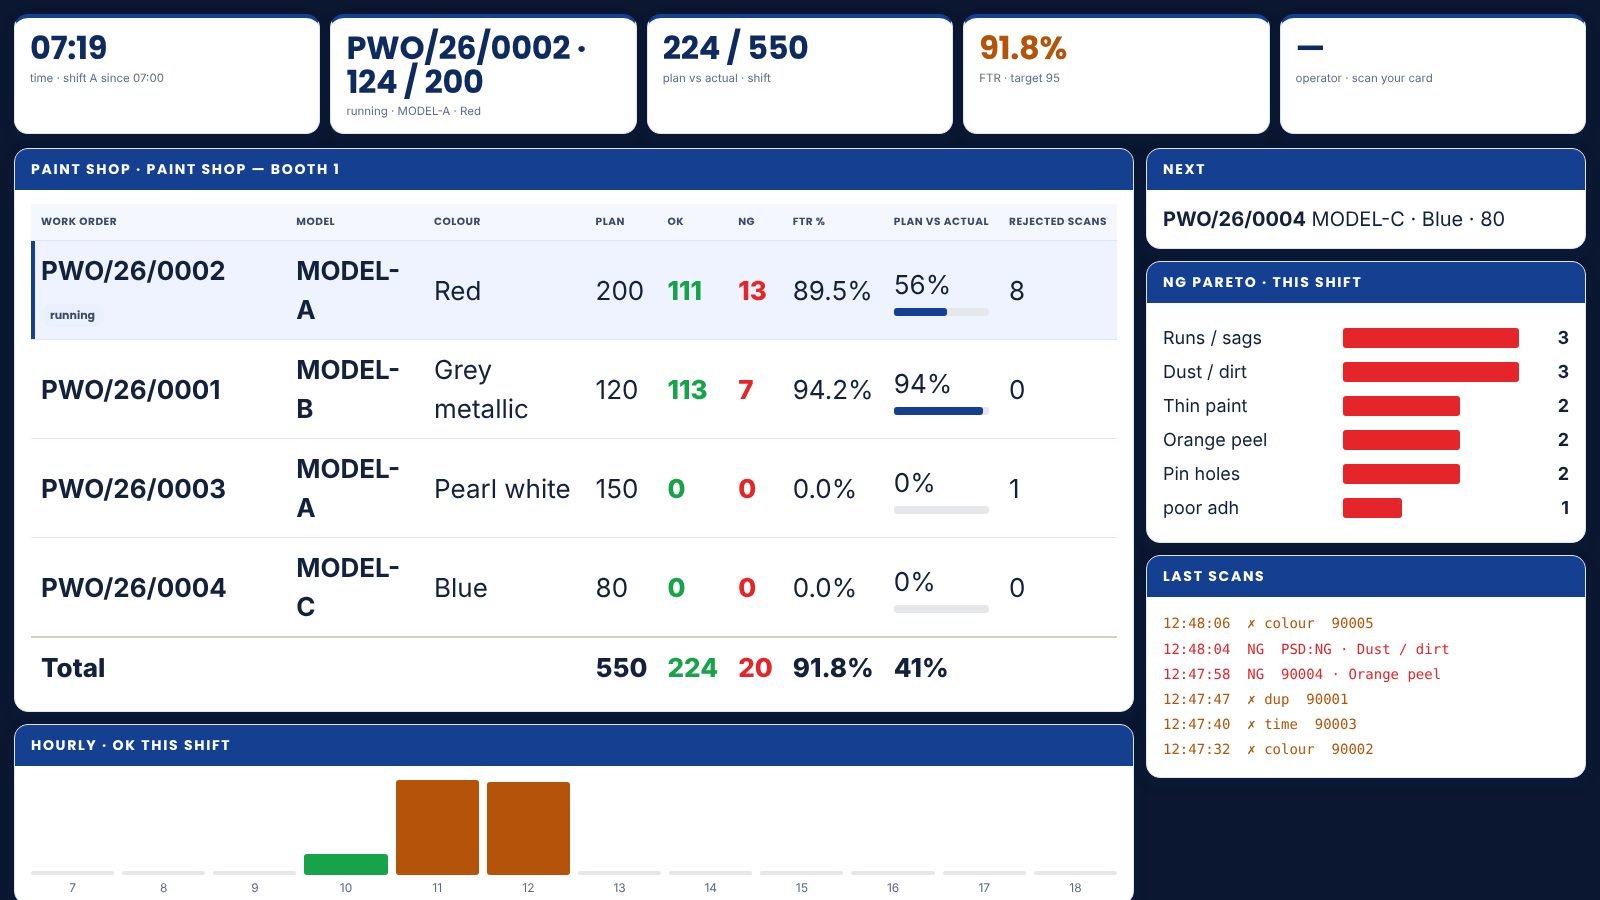
One TV per paint booth: plan, OK, NG and FTR per work order, live — every part QR checked against the running order.

A booth runs one work order at a time (model, colour, plan). Every part carries a QR with its colour and paint time; it is scanned once at unload and checked against the running order — right colour, painted within the time limit, not scanned before. A good scan counts OK by itself. For a defect the operator scans the red card and chooses the reason by stepping the list with the same scanner — no keyboard, no mouse. The TV shows plan, OK, NG, FTR, plan-vs-actual and the NG Pareto per work order; masters and plans load from Excel or CSV.
Model, colour, plan — started by card
Colour + paint time checked
OK by itself; NG with a reason by scanner
Plan, OK, NG, FTR, Pareto live
A booth runs one work order at a time (model, colour, plan). Every part carries a QR with its colour and paint time; it is scanned once at unload and checked against the running order — right colour, painted within the time limit, not scanned before. A good scan counts OK by itself. For a defect the operator scans the red card and chooses the reason by stepping the list with the same scanner — no keyboard, no mouse. The TV shows plan, OK, NG, FTR, plan-vs-actual and the NG Pareto per work order; masters and plans load from Excel or CSV.
Available as a module on the MOS platform, configured to your stations and people during installation.
Scan the work-order card at the booth: model, colour and plan are now the running order on the TV.
The part QR is checked against the order — colour, paint time, not scanned before. Pass = OK +1; fail = red screen, not counted.
Red card once opens the reason list for this model; again = next; twice = select. The last part becomes NG with that reason.
Plan, OK, NG, FTR, plan-vs-actual, NG Pareto and hourly output per work order; next order shown for the changeover.
Every figure comes from the machine, the camera or the station itself — recorded as it happens, not typed in at the end of the shift.
Scans parts and the red card — nothing else
Starts orders, approves typed reasons, watches FTR
Pareto by reason, model and colour; the scan log
Plan vs actual and FTR per booth, shift report on WhatsApp
A PC with a TV and a USB barcode scanner; the station cards printed from MOS.
A QR per part carrying colour and paint time — the format you already print, we read it as it is.
It runs on the MOS plant server; the plan and the masters come from Excel or CSV.
Models, colours and NG reasons uploaded; the first work order started by card; parts scanned and counted on the TV.
Typed reasons approved into the master; reason cards printed for the top defects; FTR target on the board.
Pareto by model and colour, plan vs actual per shift, the scan log exported for the customer audit.
The green card counts an OK by hand; it is logged as a card count, not a scan, so the report shows the difference.
Yes — each colour carries its own limit in the master; the project default applies where none is set.
No. Everything runs from the scanner; a keyboard stays in the drawer for the rare reason that is not in the list.
Every part judged by camera in under a second, defect circled.
See the module →Every machine, live — and the real reason it stopped.
See the module →Every unit scanned at every station. Nothing skips a stage.
See the module →Tell us about your plant and what you want to see. We visit, connect one machine or station, and you watch your own data in MOS before anything is quoted.